QILEE Environmental Concludes Successful Showcase of Advanced Water and Wastewater Treatment Solutions at VIETWATER 2026
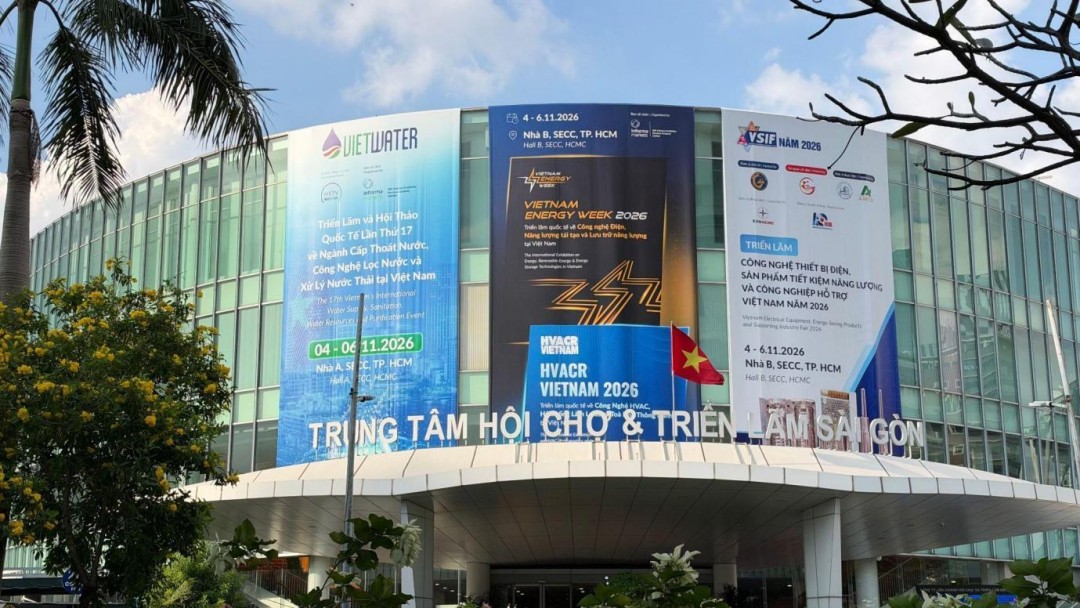
Ho Chi Minh City, Vietnam – November 16, 2026 – Shanghai QILEE Environmental Equipment Co., Ltd. (“QILEE Environmental”), a premier Chinese designer and manufacturer of specialized water treatment equipment, has officially concluded a highly successful run at VIETWATER 2026. Held from November 4 to November 7 at the Saigon Exhibition and Convention Center (SECC) in Ho Chi Minh City, the premier international exhibition served as a regional stage for QILEE Environmental to present its comprehensive line of water treatment hardware, advanced membrane separations, and integrated engineering capabilities.
Throughout the four-day event, QILEE Environmental drew significant attention from international buyers, engineering, procurement, and construction (EPC) contractors, project developers, and regional distributors. Driven by its proven technical expertise and extensive track record in custom engineering, the company secured preliminary cooperation agreements and scheduled multiple follow-up technical evaluations with industrial and municipal stakeholders.
Addressing Southeast Asia’s Industrial Transformation
VIETWATER remains one of the most prominent water utility and wastewater treatment trade platforms in Vietnam and the broader Southeast Asian region, convening equipment manufacturers, civil engineering contractors, industrial operators, and municipal water authorities.
Against a backdrop of accelerating industrialization and stricter environmental compliance mandates across Vietnam and ASEAN economies, manufacturing hubs are experiencing unprecedented demand for advanced water treatment technologies. In particular, industries face mounting pressure to deploy reliable effluent management, effluent recycling loops, zero liquid discharge (ZLD) systems for high-salinity wastewater, and infrastructure upgrades for existing municipal plants. QILEE Environmental’s participation addressed these exact operational requirements, positioning the manufacturer as an adaptable, full-spectrum solutions partner for regional clients.
Comprehensive Technology Portfolio on Display
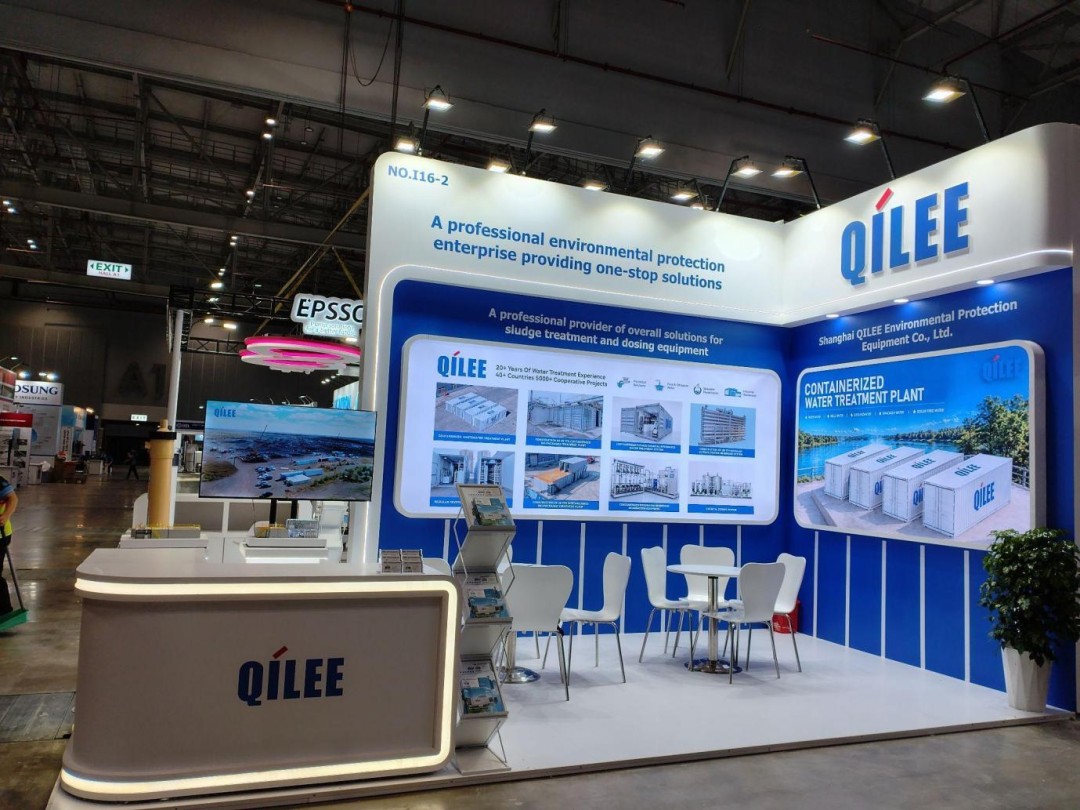
The QILEE Environmental exhibition booth served as an interactive technical hub, welcoming steady streams of corporate delegates and engineering specialists. The company highlighted an expansive portfolio of specialized treatment units engineered for demanding operating conditions, including:
- Containerized Membrane Bioreactor (MBR) Systems: Pre-assembled, space-saving decentralized treatment units that deliver high-clarity effluent suitable for non-potable reuse.
- Industrial Reverse Osmosis (RO) Units: High-recovery membrane skids optimized for pure process water preparation and advanced wastewater recovery.
- Mechanical Vapor Recompression (MVR) Evaporation & Crystallization Systems: Energy-efficient thermal separation solutions designed for high-salinity effluent and strict Zero Liquid Discharge (ZLD) compliance.
- PTFE Hollow Fiber Membrane Ammonia Removal Equipment: Rugged, chemical-resistant degasification membrane systems capable of stripping high-concentration ammonia nitrogen from challenging waste streams.
- Media Filtration & Sand Filters: Robust multi-media pre-treatment solutions engineered for suspended solids reduction and process stability.
- Automated Chemical Dosing Packages: Precision chemical metering and preparation systems tailored for flocculation, coagulation, and chemical pH adjustment.
These core technologies are designed to solve critical treatment challenges across heavily regulated sectors, such as chemical manufacturing, textile finishing, food and beverage processing, and electroplating. During technical consultations, QILEE Environmental’s engineering representatives worked directly with visitors to assess raw water quality, hydraulic load profiles, process flow selection, manufacturing lead times, and long-term maintenance cycles. The technical exchange yielded several preliminary agreements, with client-arranged site assessments slated to begin in the coming weeks.
Full Lifecycle Support and Regional Expansion
As a seasoned environmental equipment manufacturer, QILEE Environmental has maintained a sustained commitment to expanding its Southeast Asian operations. The company distinguishes itself by providing end-to-end lifecycle execution, integrating process flow modeling, precision in-house equipment fabrication, overseas installation supervision, and on-site commissioning.
VIETWATER 2026 served as a pivotal milestone in strengthening QILEE Environmental’s regional distributor network and enhancing collaboration with local EPC firms. By working with in-market agents, the company aims to offer responsive after-sales service, rapid spare-parts distribution, and local technical assistance.
Sustained Commitment to Sustainable Development
While the four-day trade event has wrapped up, QILEE Environmental’s commercial and technical engagements in Vietnam continue to expand. Moving forward, the company plans to further optimize its modular, compact, and low-maintenance equipment lines to suit Southeast Asia’s tropical climate and industrial footprint. These targeted configurations help regional enterprises adhere to strict environmental standards, lower lifecycle operating costs, and reclaim critical water resources.
As part of its ongoing internationalization strategy and alignment with green industrial development under the Belt and Road Initiative, QILEE Environmental will continue participating in prominent environmental conferences worldwide, introducing field-proven, dependable wastewater engineering solutions to emerging markets.
Inquiries can be sent on WhatsApp at +86 13636655908 or email [email protected]
Learn more at: https://www.qileegroup.com/
About QILEE Environmental
Shanghai QILEE Environmental Equipment Co., Ltd. is an established Chinese manufacturer and technical service provider specializing in comprehensive water and wastewater treatment solutions. With extensive experience in environmental machinery design and process engineering, QILEE Environmental manufactures and supplies containerized MBR systems, reverse osmosis skids, MVR evaporation and crystallization setups, specialized PTFE membrane degasification units, and modular chemical dosing packages. Serving diverse industrial sectors, including textiles, electroplating, chemical processing, and food production, as well as municipal utilities, QILEE Environmental delivers dependable turnkey support encompassing design, fabrication, installation supervision, and on-site commissioning worldwide.
For more information, visit qileegroup.com.
Media Contact
Company Name: QILEE
Contact Person: Tina
Email: Send Email
Phone: +86 13370035529
City: Shanghai
Country: China
Website: qileegroup.com


